Ningbo Empire · Engineering & manufacturing
Inspection and quality records.
Dimensional, magnetic and functional checks defined for your production program.
Review the original documentation.
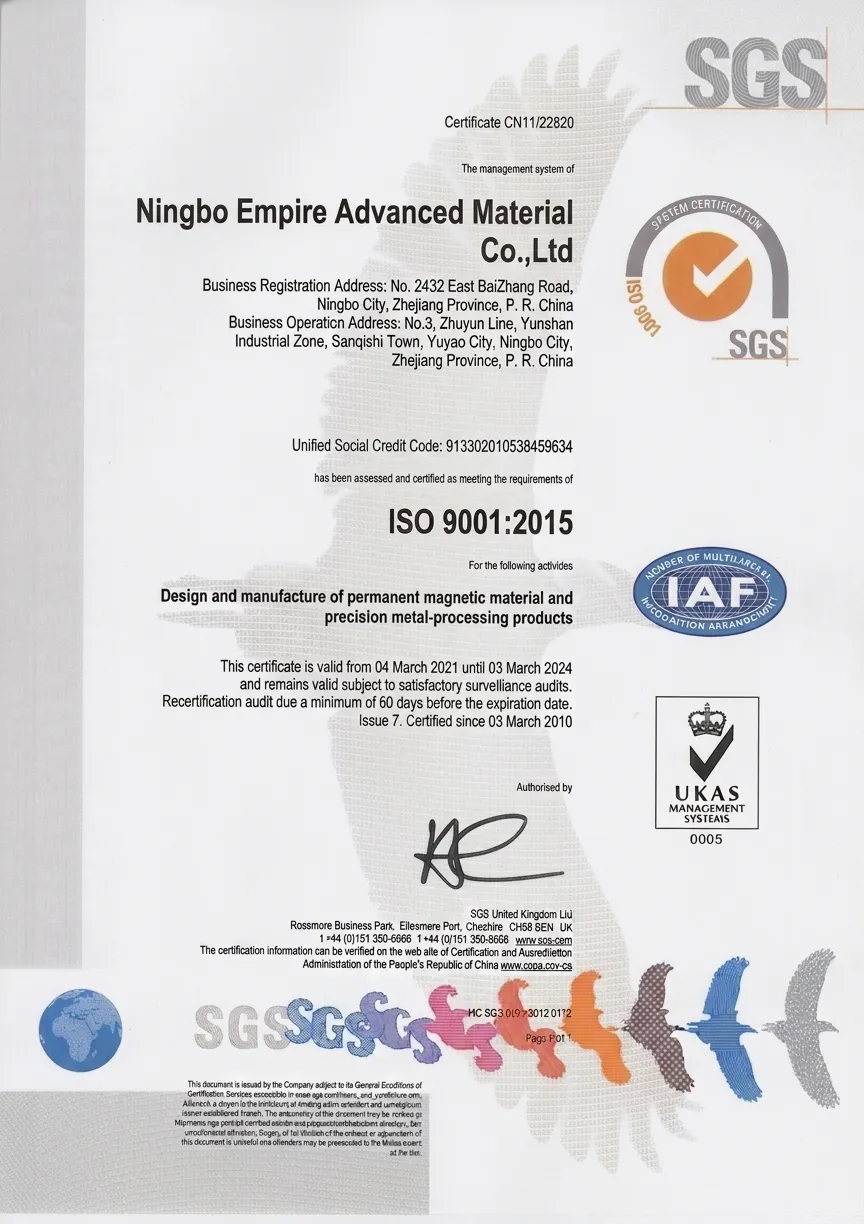
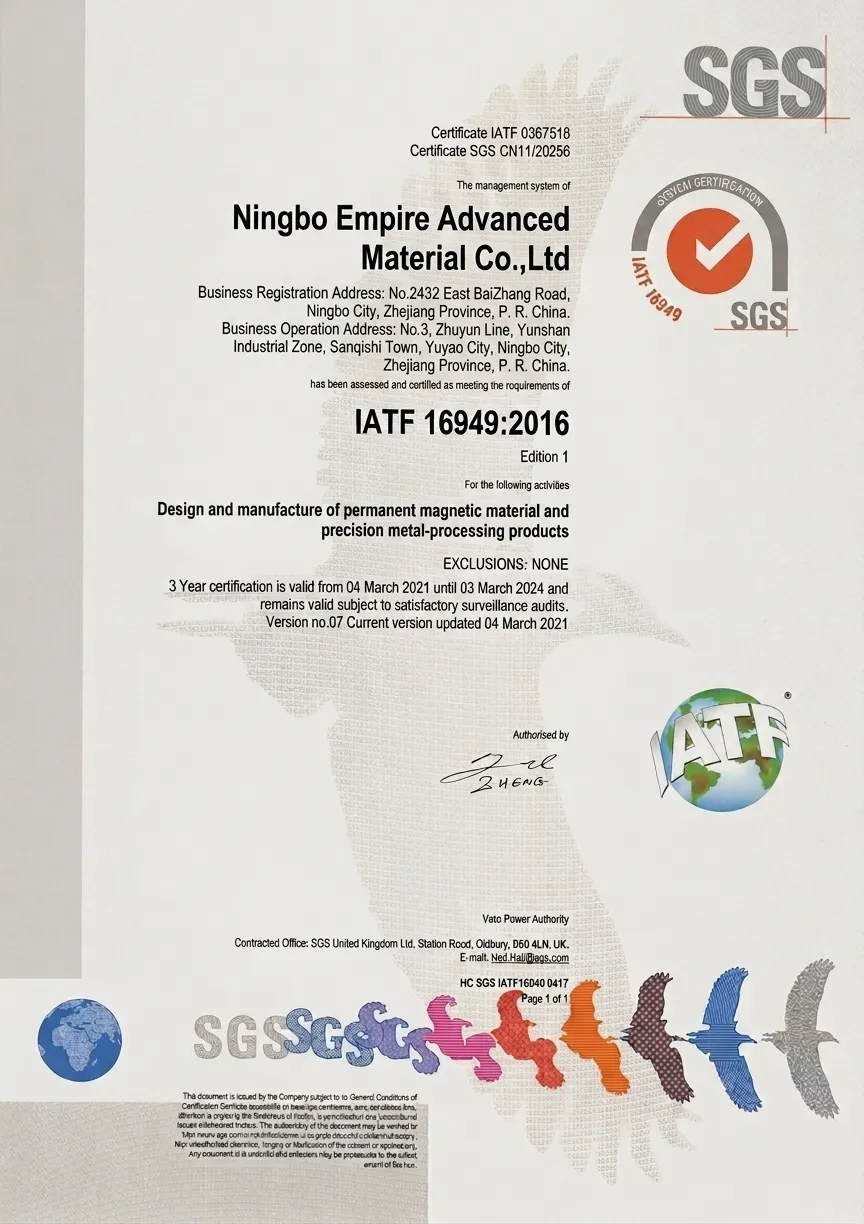
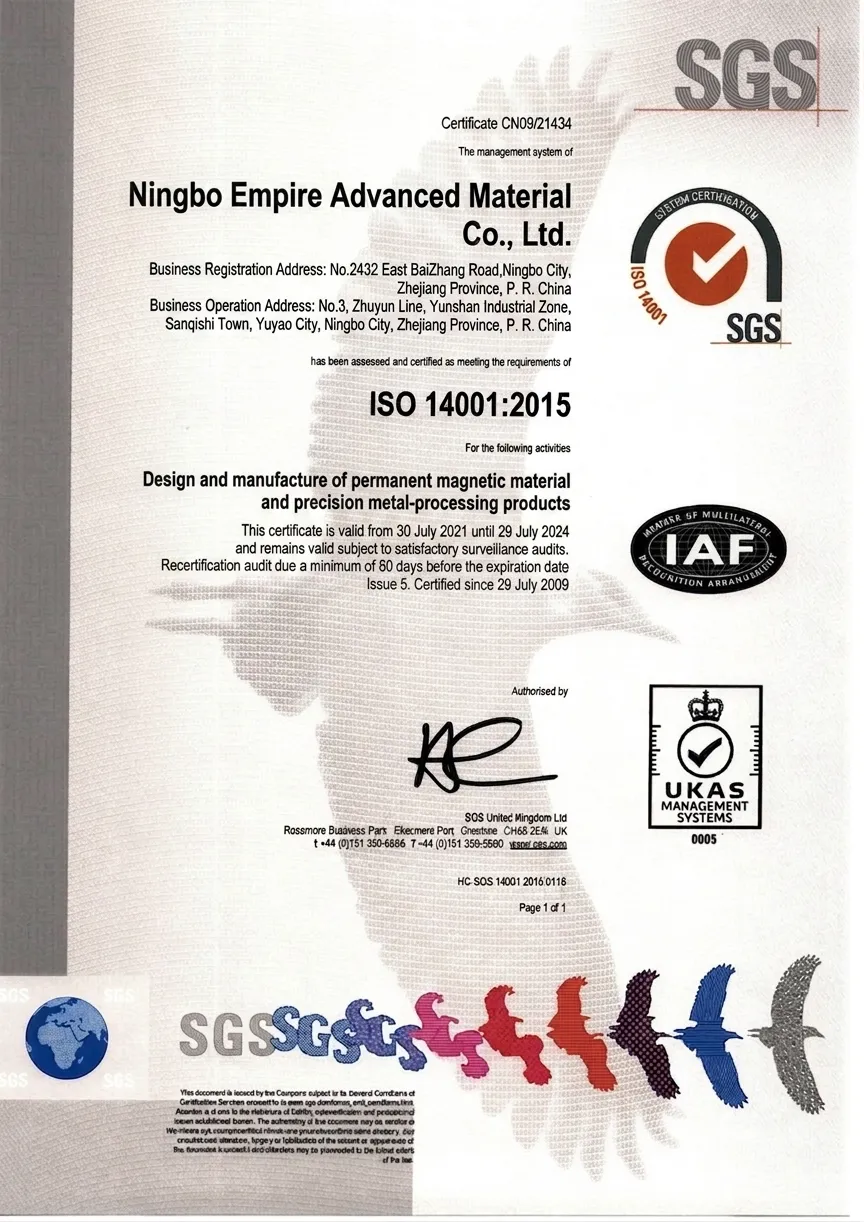
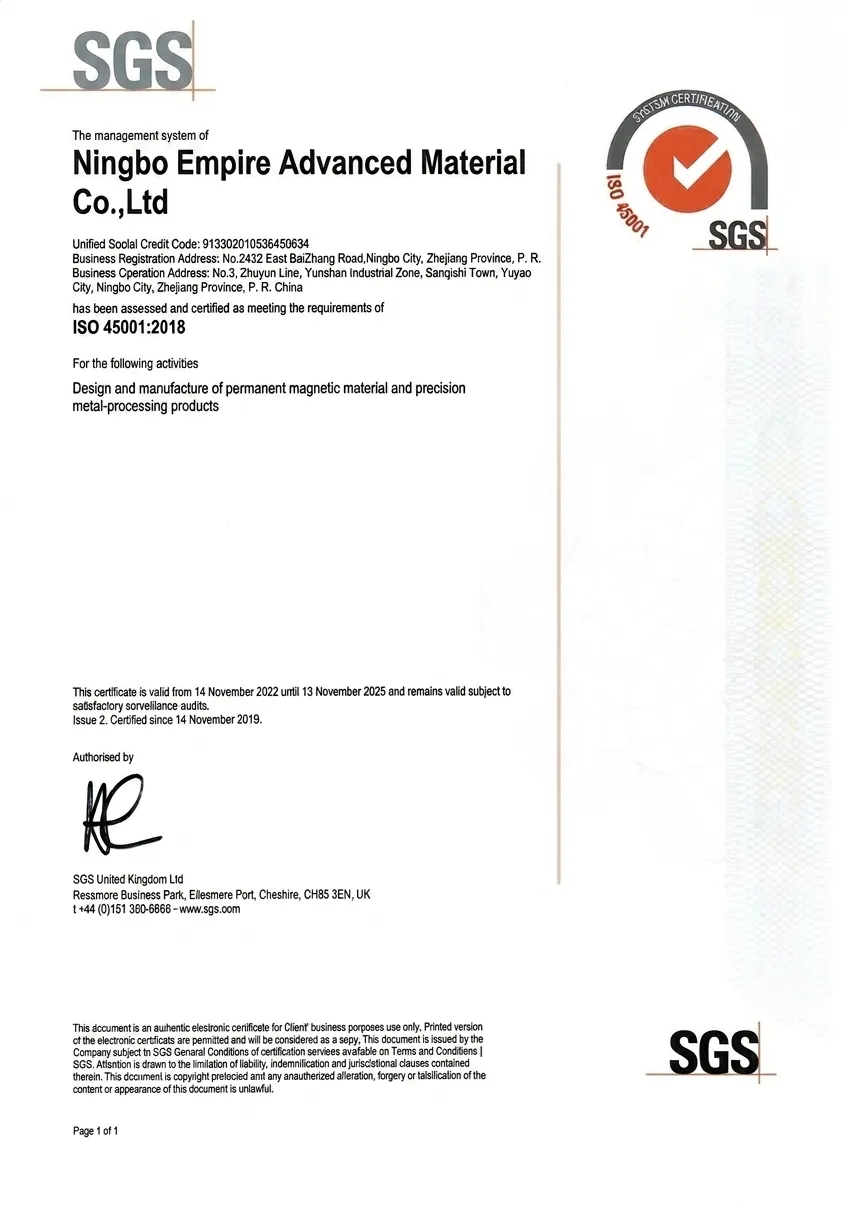
Certificate holders, registration numbers, scopes and quality controls
IATF 16949:2016
Open IATF 16949:2016ISO 14001:2015
Open ISO 14001:2015ISO 45001:2018
Open ISO 45001:2018Certificate records identify Ningbo Empire Advanced Materials Co., Ltd. (USCC 913302010538459634). Current status and producing-site scope are confirmed during quotation.
Quality Management System
- Holder
- Ningbo Empire Advanced Material Co., Ltd.
- Registered address
- #2432 East BaiZhang Road, Ningbo, China 315040
- Cert No.
- CN11/22820 (SGS)
- Scope
- Design and manufacture of permanent magnetic material and precision metal-processing products
Automotive Quality Management
- Holder
- Ningbo Empire Advanced Material Co., Ltd.
- Registered address
- #2432 East BaiZhang Road, Ningbo, China 315040
- Cert No.
- IATF 0367518 / SGS CN11/20256
- Scope
- Design and manufacture of permanent magnetic material and precision metal-processing products
Environmental Management
- Holder
- Ningbo Empire Advanced Material Co., Ltd.
- Registered address
- #2432 East BaiZhang Road, Ningbo, China 315040
- Cert No.
- CN09/21434 (SGS)
- Scope
- Design and manufacture of permanent magnetic material and precision metal-processing products
Occupational Health & Safety
- Holder
- Ningbo Empire Advanced Material Co., Ltd.
- Registered address
- #2432 East BaiZhang Road, Ningbo, China 315040
- Cert No.
- SGS ISO 45001 (USCC 913302010538459634)
- Scope
- Design and manufacture of permanent magnetic material and precision metal-processing products
Which sites do these certificates cover? The registered address on the cards identifies the company office. Each original certificate scan states its certified operating address and activities. For a specific part number or program, the producing site and its applicable certificate scope are confirmed during qualification. Strategic manufacturing bases are assessed under their own quality systems.
Our Quality Process
- Incoming controls — raw materials are verified according to the applicable control plan before production release.
- In-process controls — critical dimensions and functional properties are monitored at defined production stages.
- Final inspection — visual, dimensional and functional checks follow the agreed inspection plan and lot requirements.
- CMM verification — coordinate measuring machine reports for complex geometries and tight tolerances.
- Traceability — lot and production records are maintained according to product and program requirements.
- Pre-shipment video inspection — recorded or live video review of finished goods, labeling and packaging before dispatch, available on request.
Documentation We Provide
Review the inspection, material and project records below, then agree the documentation required for your part.
Review project-specific recordsDimensional and functional inspection.
Assembly testing
Assembly checks and agreed test records.
Dimensional inspection
Coordinate measurement and dimensional records.
Optical inspection
Microscope inspection for LTCC material evaluation.
Internal features
X-ray inspection of die-cast components, where required.
Incoming material
Verify against the control plan.
In-process checks
Monitor critical features.
Final inspection
Release against agreed criteria.
Lot traceability
Connect parts to production records.
Keep the test conditions with the result.
For composition and coating records, identify the material lot, analysis method, coating system, measurement positions and acceptance limits. For magnetic results, keep temperature, conditioning, drawing datum, orientation, fixture, units and sample count with the Br / Hcj or field-distribution record.
Agree HAST, neutral salt spray or the specified pressure-cooker method separately. Record specimen and coating condition, temperature, pressure, humidity, duration and the measured acceptance criterion. A named test requirement does not establish that every producing site owns the same instruments.
Review coating reference conditions · Agree the inspection and producing-site scope
Agree the records before production.
| PPAP (per project) | Production part approval package for automotive and regulated industries, to the level agreed with your SQE |
|---|---|
| FAI Reports | First Article Inspection against the agreed drawing and reporting scope |
| Material Certs | Mill certificates, chemical composition reports, and material traceability |
| Magnetic Test Data | Flux, BH-curve and pull-force results as specified in the agreed test plan |
| RoHS / REACH | Product-specific substance declarations and supporting records, as available for the agreed scope |
| CMM Reports | Dimensional inspection data for machined and assembled parts |
Testing Capabilities
Magnetic properties
BH-curve, flux and force checks against the selected material requirements.
Dimensional inspection
Critical dimensions checked against the drawing and inspection plan.
Optical measurement
Non-contact measurements for small profiles and features.
Magnetic field mapping
Field-pattern inspection for the specified magnetization.
Environmental checks
Salt-spray, humidity and thermal-cycle requirements are agreed for the coating and application.
Defined acceptance
Agree dimensions, material properties, functional checks, sampling and report format.
Project documentation
Information to Include in Quality Records
Use these document fields to plan the inspection record for the approved part.
First-article record
Part number · drawing revision · material/lot · drawing characteristic · nominal and tolerance · measured result · method · disposition.
Batch & material record
Lot reference · grade/material designation · applicable test method · certificate or analysis results · traceability reference · release status.
Change-control record
Changed material, process or location · affected parts · reason · validation plan · customer approval · effective lot.
Discuss Your Documentation RequirementsQuality documentation & supplier review
Identify the producing site, part number and required record package when requesting documentation.